
CNC Pipe Bending Machine
Specify DW CNC bending from the complete programmed part, feed/turn requirements and controller type. Approve tooling and finished geometry before repeat output.
- Source models
- 14 rows
- Motion functions
- Feed / turn / bend
- Max angle reference
- 190°
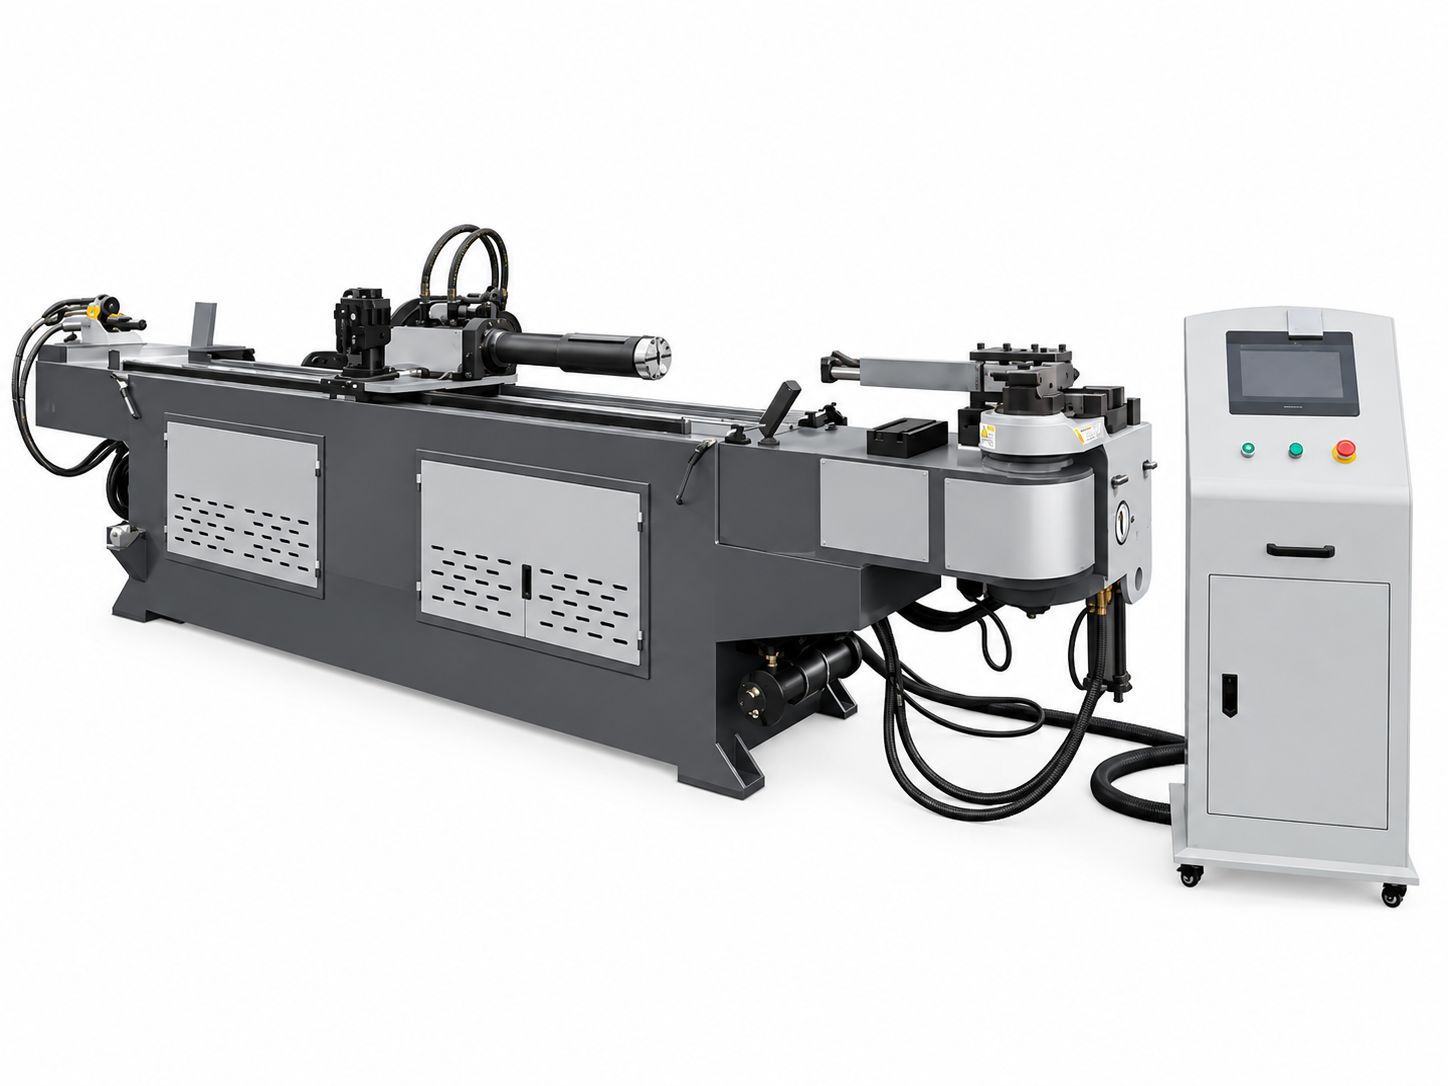
Three movements make the programming discussion concrete
Feed, turn and bend
The DW CNC source describes programmable bending with servo-controlled tube turning and feeding. Confirm the selected model’s complete motion package and sequence.
A multi-plane workpiece needs more than a bend-angle list. Send straight lengths, rotation planes and the complete finished geometry, including the positions that are difficult to clamp or support.
Choose the data and controller route
| Function | PLC type | Industrial-computer type |
|---|---|---|
| Number of bends | 16 pcs | 33 pcs |
| Stored part programs | 1000 sets | 50,000 sets |
| Data entry | X/Y/Z or Y/B/C source modes | Confirm supplied input and programming workflow |
These are controller-type references, not included features of every order. Confirm controller type, version, language, program entry and any offline software in the quotation.
Two catalog rows deserve explicit confirmation
Build a real multi-bend acceptance sequence
- 01
Provide the complete drawing
Specify actual material, tube size and dimensional criteria.
- 02
Agree tools and feed mode
Review direct/indirect feed, clamping and support.
- 03
Program and trial
Include rotations, short straight sections and successive bends.
- 04
Inspect the whole part
Check angles, endpoint dimensions and deformation.
- 05
Repeat the batch
Record setup changes, loading and acceptable finished parts.
Fourteen DW CNC Model References
Open the complete supplied model table
| Model | Max. Bending Diameter / Wall Thickness | Max. Bending Radius (mm) | Max. Bending Angle (°) | Max. Feeding Length (mm) | Feeding Mode | Pipe Bending Speed (°/s) | Pipe Turning Speed (°/s) | Feeding Speed (mm/s) | Pipe Bending Precision (°) | Pipe Turning Precision (°) | Feeding Precision (mm) | Pipe Turning Servo Motor (kW) | Feeding Servo Motor (kW) | Hydraulic Motor Power (kW) | Max. System Pressure (MPa) | Machine Weight (kg) |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| DW-18CNC | Φ18×1.2 | R120 | 190 | 1800 | Direct or Indirect Feed | Max 180 | Max 200 | Max 1000 | ±0.1 | ±0.1 | ±0.1 | 0.2 | 0.4 | 4 | 10 | 1200 |
| DW-25CNC | Φ25×1.5 | R160 | 190 | 2000 | Direct or Indirect Feed | Max 150 | Max 200 | Max 1000 | ±0.1 | ±0.1 | ±0.1 | 0.4 | 0.75 | 4 | 10 | 1200 |
| DW-38CNC | Φ38×2 | R180 | 190 | 2200 | Direct or Indirect Feed | Max 150 | Max 200 | Max 1000 | ±0.1 | ±0.1 | ±0.1 | 0.75 | 1 | 4 | 12 | 1300 |
| DW-58CNC | Φ50×2 | R180 | 190 | 3000 | Direct or Indirect Feed | Max 150 | Max 200 | Max 1000 | ±0.1 | ±0.1 | ±0.1 | 0.75 | 1.5 | 4 | 12 | 1500 |
| DW-50CNC | Φ60×3 | R250 | 190 | 3000 | Direct or Indirect Feed | Max 85 | Max 200 | Max 1000 | ±0.1 | ±0.1 | ±0.1 | 0.75 | 1.5 | 5.5 | 12 | 2500 |
| DW-63CNC | Φ63×4 | R250 | 190 | 3000 | Direct or Indirect Feed | Max 85 | Max 200 | Max 1000 | ±0.1 | ±0.1 | ±0.1 | 1 | 1.5 | 5.5 | 12 | 3000 |
| DW-75CNC | Φ75×4 | R300 | 190 | 3000 | Direct or Indirect Feed | Max 40 | Max 160 | Max 800 | ±0.1 | ±0.1 | ±0.1 | 1.5 | 2 | 7.5 | 12 | 4500 |
| DW-89CNC | Φ89×6 | R300 | 190 | 3000 | Direct or Indirect Feed | Max 30 | Max 160 | Max 800 | ±0.1 | ±0.1 | ±0.1 | 2 | 3 | 11 | 14 | 5500 |
| DW-114CNC | Φ114×8 | R450 | 190 | 3000 | Direct or Indirect Feed | Max 30 | Max 160 | Max 800 | ±0.1 | ±0.1 | ±0.1 | 2 | 3 | 22 | 14 | 6800 |
| DW-130CNC | Φ130×8 | R450 | 190 | 3000 | Direct or Indirect Feed | Max 30 | Max 160 | Max 800 | ±0.1 | ±0.1 | ±0.1 | 2 | 3 | 22 | 14 | 7800 |
| DW-168CNC | Φ168×14 | R600 | 190 | 3500 | Direct or Indirect Feed | Max 30 | Max 160 | Max 800 | ±0.1 | ±0.1 | ±0.1 | 3 | 4 | 35 | 14 | 12000 |
| DW-219CNC | Φ219×16 | R800 | 190 | 4000 | Direct or Indirect Feed | Max 30 | Max 80 | Max 600 | ±0.2 | ±0.1 | ±0.1 | 3 | 5 | 35 | 14 | 22000 |
| DW-273CNC | Φ273×20 | R800 | 190 | 4000 | Direct or Indirect Feed | Max 25 | Max 80 | Max 500 | ±0.2 | ±0.1 | ±0.1 | 3 | 7 | 35 | 14 | 25000 |
| DW-325CNC | Φ325×30 | R1200 | 190 | 5000 | Direct or Indirect Feed | Max 20 | Max 60 | Max 500 | ±0.2 | ±0.1 | ±0.1 | 7 | 11 | 55 | 14 | 38000 |
The source lists bending precision ±0.1° for most rows and ±0.2° for DW-219CNC, DW-273CNC and DW-325CNC. These and feed/turn figures do not establish unconditional whole-part tolerance. Agree test conditions and actual finished-part acceptance.
Keep the common configuration reference
The source describes servo bending on applicable configurations and hydraulic bending for larger configurations. CNC control alone does not prove all-electric bending, a particular axis count or every tool on the supply list.
Feeding length, radius and speed are separate limits
Usable feed arrangement
Review the listed feed length with tube loading, clamping and the chosen direct or indirect feed mode. Confirm the complete workpiece reach.
Radius and tooling
A listed maximum radius does not define the minimum bend radius. Obtain the actual die and support-tool review.
Completed-part cycle
The table gives separate maximum feed, turn and bending speeds. Do not combine them into a guaranteed parts-per-hour figure.
Questions to settle before ordering
Are 33 bends and 50,000 programs standard?
They are industrial-computer-type references. Confirm the controller package; the PLC references differ.
Are the DW-58CNC and DW-50CNC size labels consistent?
Their source OD entries appear mismatched with their names. Obtain model-specific confirmation rather than silently changing the table.
Is every CNC machine all-electric?
No. The source describes both servo and hydraulic bending configurations.
Does ±0.1° guarantee every finished part dimension?
No. Whole-part acceptance depends on the actual stock, tooling, setup and sequence.
What is needed for a CNC production trial?
Full geometry, grade, OD, wall, radius, rotation sequence, critical dimensions and the batch mix.
Tell Us Your CNC Tube Bending Requirements
Send tube material, outside diameter, wall thickness, bending radius, feeding length and workpiece drawing so we can confirm the suitable CNC model and tooling.